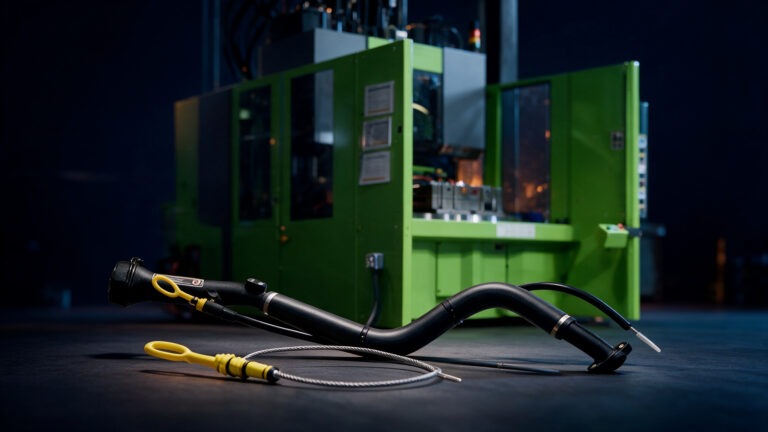
There’s a moment during every OEM program that decides whether launch day goes smoothly or turns into a scramble: the moment parts hit the production line. When a part arrives finished, welded, decorated, assembled, tested, and ready to install, that moment is a non-event. Nobody remembers it, because nothing went wrong. That quiet, uneventful outcome is the entire point of plastic welding and assembly done right, and it’s the difference between a supplier who ships parts and a value-added partner who ships a finished component.
Getting there means a lot has to happen before the part ever reaches your production line. Welding, decorating, assembly, and testing each come with their own methods and standards, and getting any one of them wrong can turn a routine step into a delay. These secondary operations, more than the molding itself, are where that outcome gets built, or lost.
What Are Secondary Operations in Plastic Injection Molding?
Secondary operations are the manufacturing steps that happen after a part comes out of the mold and before it ships as a finished product: welding, decorating, assembly, and the testing that verifies it all. A molded part on its own is rarely the end product an OEM needs; secondary operations are what close that gap.
Plastic Welding Methods: Choosing the Right Process
Plastic welding joins two or more molded parts into a single sealed or structural assembly, without adhesives or mechanical fasteners. The four methods below cover most OEM applications, but they are not interchangeable. The right one depends on part geometry, joint accessibility, and what the assembly needs to withstand once it’s in the field.
Ultrasonic Welding
Ultrasonic welding uses high-frequency vibration to generate localized heat at the joint line, fusing the parts in seconds. It’s the fastest of the four methods and works well for small to mid-size parts with simple, accessible joint geometry. On a high-volume program, those saved seconds compound. A few seconds per part, multiplied across a long production run, add up fast, without sacrificing joint integrity.
Vibration Welding
Vibration welding uses friction, generated by vibrating one part against another under pressure, to melt and fuse the joint surface. It handles larger parts and irregular or contoured joint lines that ultrasonic tooling can’t reach. That means an engineer isn’t forced to simplify a part’s geometry just to make it weldable.
Spin Welding
Spin welding joins round or cylindrical parts by rotating one against the other under pressure until friction generates enough heat to fuse the joint. It’s a simple, repeatable process for parts like caps, housings, and fluid reservoirs, and repeatable is the point. A circular joint welded this way performs the same on part one as it does on part ten thousand.
Hot Plate Welding
Hot plate welding heats the joint surfaces of both parts directly with a heated plate, then presses them together to fuse. It handles large parts, dissimilar wall thicknesses, and joints that need a fully sealed, leak-tight result. That’s why it shows up most often on fluid reservoirs and enclosures that have to hold a seal under real pressure or vibration.
Decorative Printing and Functional Marking: Branding and Traceability
Pad printing and hot foil stamping put logos and brand elements directly onto a molded surface, including curved or textured surfaces that standard printing can’t reach. That’s what turns a generic molded part into something branded, without adding a separate vendor or shipping leg to the process.
Laser marking and barcode label printing handle the identification side. Laser marking etches part numbers, warning labels, and calibration marks directly into the surface, permanent marks that hold up over the life of the part. Barcode labels get printed and applied for lot tracking and traceability, giving each part a scannable record tied back to its production run.
Assembly Services: Turning Many Parts Into One Finished Unit
Assembly is where welded, decorated, and molded parts come together into a finished unit. RL Hudson’s in-house assembly department combines automation with skilled employees to handle varying production volumes and build complexity, from small, simple assemblies to high-volume, multi-component programs. That’s part consolidation in practice. Instead of managing separate shipments, handoffs, and the risk of something going missing along the way, an OEM gets one part number, already checked for fit and function before it ships. That verification is work the OEM would otherwise have to do itself once the pieces arrived.
Verifying the Joint: Quality Testing on Welded and Assembled Parts
A welded joint that looks fused and a welded joint that holds under pressure are not always the same thing. That gap is why testing happens after welding and assembly, not just after molding.
Leak testing checks whether a joint actually holds a seal, which matters most on parts built to perform under pressure in the field, like fluid reservoirs and sealed enclosures. Pull, tensile, and burst testing go a step further, confirming the joint has the mechanical strength the application actually needs, not just the appearance of being fused. Dimensional inspection closes the loop, confirming the finished assembly still holds tolerance after welding, not just coming out of the mold. Depending on the part, that inspection is run manually, on a CMM, or through vision-based systems.
This testing runs under the same IATF 16949 quality system as the rest of the operation, so the data an OEM eventually needs is typically already on file rather than something to chase down later. Error proofing runs throughout the process rather than waiting for a final check, reflecting the zero-defect mindset behind the sector’s 0 PPM goal.
In Practice: Fifty-Eight Parts, One Finished Assembly

Exploded view illustrating how multiple molded components and hardware come together into a single finished assembly.
This is what that non-event moment looks like in practice. A heavy-duty diesel engine manufacturer needed a breather assembly for one of its engine platforms, built from 16 unique components and 58 pieces in total. Rather than shipping those pieces out to be assembled somewhere else, RL Hudson molds the cover and base; installs thread inserts using robot-assisted heat staking; installs the compression limiters, other purchased parts, and sensors; and finishes every other operation the part needs, all under one roof.
Before it ships, the assembly runs through two dedicated leak test stations. Every part is serialized, and every operation along the way is traceable, the kind of documentation a zero-defect mindset actually requires, not something added on at the end.
The OEM isn’t juggling 58 pieces across 16 part numbers, hoping nothing goes missing or gets mismatched along the way. It’s getting one part number, fully documented and ready to install, with a single team standing behind it instead of dozens of pieces with no one accountable for the whole.
Why OEMs Choose RL Hudson’s Secondary Operations for Program Success
RL Hudson runs molding, welding, assembly, and testing under one roof, governed by a single IATF 16949 quality system. For an OEM, that means the team that built your part is the same team that welded it, assembled it, and tested it, so nothing gets lost in a handoff between companies, and there’s one place to go if something needs to be traced back. That continuity is what actually protects a program. There’s no coordinating across separate schedules, no re-explaining the part to a team that didn’t build it, no waiting on someone else’s answer. It’s one team that already knows the part, working it from start to finish, which is what keeps a launch date a launch date instead of a moving target.